Project Cases
Successful Conveyor Solutions
 2026-08-11
Dairy Processing Line Retrofit
Retrofitted an existing dairy processing line with new modular belts and chain guides, improving efficiency by 30% and reducing maintenance downtime.
 2026-08-11
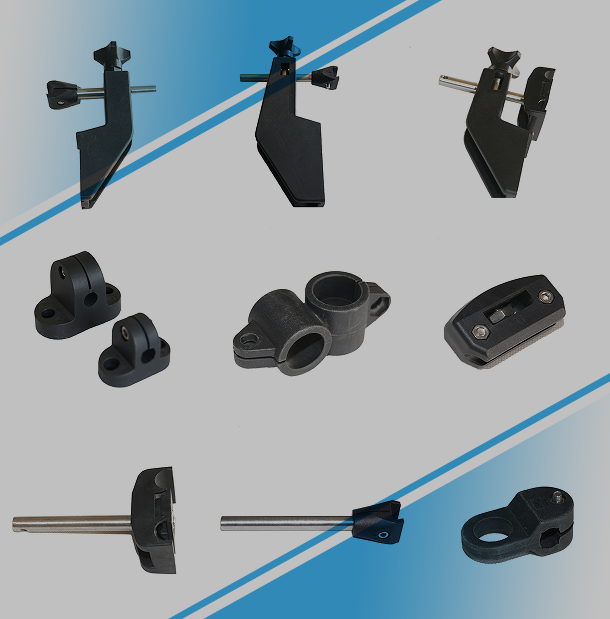
Electronics Manufacturing Clean Conveyor
Provided ESD-safe conveyor components and chain systems for an electronics manufacturing facility, ensuring static-free product transport.
 2026-08-11
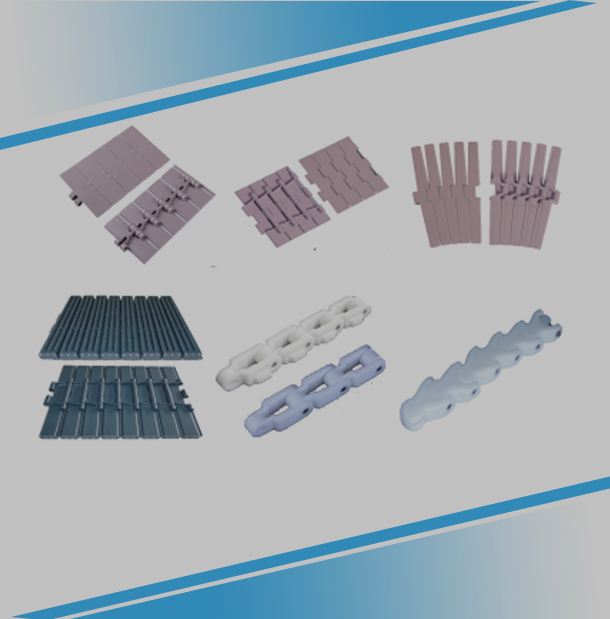
Bakery Production Conveyor Network
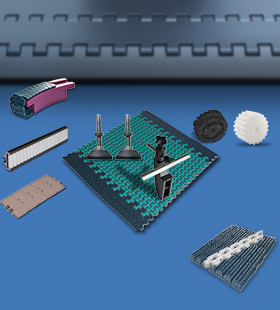
Installed a comprehensive conveyor network for a large-scale bakery, integrating plate top chains and 1873TAB series for gentle product handling.
 2026-08-11
Logistics Sorting Center Upgrade
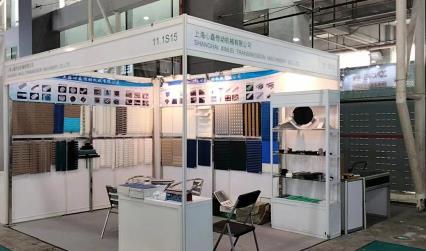
Large-scale conveyor system deployment for a logistics sorting center, featuring modular belts, corner tracks, and wear strips for 24/7 operation.
 2026-08-11
Pharmaceutical Clean Room Conveyor System: Meeting FDA & GMP Standards
Designed and installed a hygienic conveyor system for a pharmaceutical clean room environment, using stainless steel chains and FDA-compliant materials.
 2026-08-11
Food Packaging Modular Belt Installation
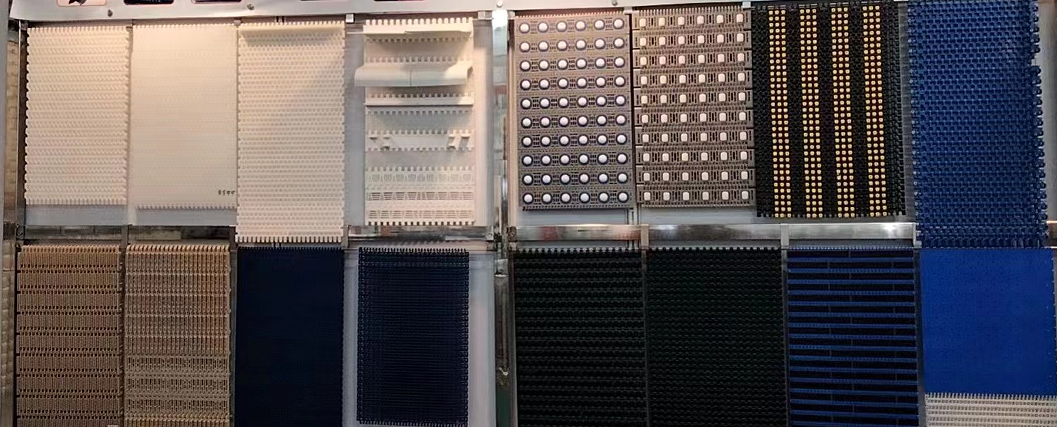
Custom modular belt solution for a food packaging facility, implementing X2500 series belts for heavy-duty frozen food handling with superior impact resistance.
 2026-08-11
Automotive Parts Assembly Line
Engineered and delivered a complete metal flat top chain system for an automotive parts manufacturer, including 812 series chains and custom sprockets.
 2026-08-11
Beverage Bottling Line Conveyor System
Complete conveyor system upgrade for a major beverage bottling plant, featuring RT114 case chains and 820 series flat top chains for high-speed bottle conveying.